


International Brands We Collaborate With


Features of ChillerOne Food Processing Chillers
- Equipped with a system that can control the temperature in real time, it can adjust and lock in the optimal cooling temperature in real time.
- Combining the dual energy-saving systems of air cooling and water cooling lessens energy consumption and improves efficiency.
- No need to continuously purchase and add ice, radically reducing material and labor costs, with a one-time investment and long-term peace of mind.
- Built-in ethylene glycol anti-freeze system and enhanced anti-freezing design, lowering the risk of shutdown and guaranteeing smooth production around the clock.
- Deeply supports customized services. Whether it’s the food processing procedures or the site restrictions, we can offer corresponding solutions.
ChillerOne — Your Reliable Food Processing Chillers Supplier
The cooling process is the core of food and beverage production, as it directly determines the freshness, safety, and commercial value of the products. A professional food processing chiller guarantees that every step, from raw material processing, fermentation and brewing, rapid freezing to constant temperature storage, is within the optimal process window.
At ChillerOne, our chillers are specifically designed to meet the stringent requirements of food processing. If you need them, please feel free to contact us. We will provide you with a matching refrigeration solution.
The Types of Chillers Applied in Food Processing

The drinking water chiller uses pure water as the circulating medium. Its core adopts a double-layer plate heat exchanger to conduct complete physical isolation, guaranteeing that the cooling water has no cross-risk with the food production line. This system operates well in the temperature range of 0°C to 15°C, can remove production heat, and is especially suitable for dairy processing with strict hygiene requirements, rapid cooling after sauce cooking, and central kitchen meal preparation lines etc. For you, it combines high cost-effectiveness with food safety assurance, meeting daily large-scale cooling needs and operating energy consumption.

It uses food-grade propylene glycol as the coolant. By adjusting the concentration, the operating temperature can be extended to -5°C or even -30°C. Its key advantage is eliminating the risk of pipeline freezing, making it ideal for cold environments and continuous, all-day production. The system enables precise temperature and process control and is widely applied in ice cream freezing, chocolate continuous temperature control, beer fermentation tank cooling, and low-temperature meat processing. It provides a reliable quality foundation for high-value products, ensuring consistent quality and high yield in every batch.

Air-cooled chillers are an independent refrigeration unit that relies on air for heat dissipation. Its design integrates the compressor, evaporator, and finned condensing fan into a modular unit, without the need for an external cooling tower. This structure brings great flexibility according to deployment, and can be quickly installed and used in well-ventilated areas. This saves machine room space and complex piping engineering. It is suitable for factories that lack water sources or others that wish to lower water treatment costs. The low maintenance and stable production are affordable cooling solutions for many industrial applications.

This is a cooling solution that effectively dissipates heat through a cooling tower and water circulation. Due to its ability to control the condensation temperature with efficiency, its energy efficiency is usually greatly higher than that of air-cooled chillers, and the energy-saving advantage is more obvious in long-term continuous operation. This system is suitable for central refrigeration station design, where a single unit can meet extremely high cooling capacity needs and can offer cold sources for numerous production lines and different process sections within the factory through stable, low-temperature water or ethylene glycol solution.
Reliable Certification
Made in accordance with universal food industry specifications, the chillers provide ideal thermal conditions for standardised food manufacturing.


Application in the Food Processing Industry
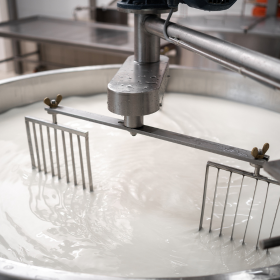
In dairy product production, temperature is crucial for its taste and safety. Our industrial refrigeration system can provide a precise and stable temperature range from +40℃ to -40℃. Whether it is the rapid pre-cooling of fresh milk, the constant temperature control during yogurt fermentation, the slow maturation of cheese curds, or the rapid freezing of ice cream, our chiller can guarantee that each stage is in the best condition. Its independent sanitary circuit design can lower the risk of contamination, which can help your product to gain market trust in terms of taste, texture, and shelf life.
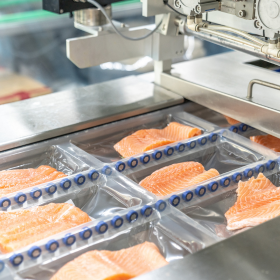
The cause of spoilage of meat and seafood is the increase in temperature. We have a powerful and rapid freezing and deep refrigeration area. After slaughter or fishing, the chiller can immediately reduce the core temperature of the product to -18℃ or even below -30℃, quickly inhibiting microbial activity. Whether it is for pre-cooling on the production line or advanced processes like single-piece rapid freezing, our system can guarantee that the product’s cell structure is intact and the loss of juice is minimized, then your products can extend their shelf life while guaranteeing food safety and creating the best product appearance.
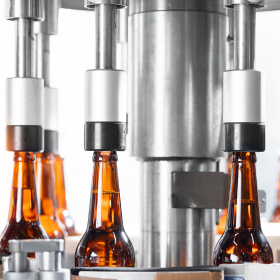
In beer and wine brewing, our ethylene glycol cooling system can provide precise temperature control within ±0.5℃ for your fermentation tanks, guaranteeing pure and stable fermentation flavors. Before filling juices, teas, and carbonated beverages, the rapid cooling system can remove heat, guaranteeing the freshness of the filled products.
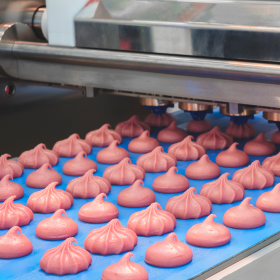
During the production of chocolate and candies, our specially designed temperature control cooling system can precisely execute complex temperature rise and drop curves, guaranteeing that the chocolate has a bright appearance and a crisp breaking effect. In the baking field, our equipment can be used for cooling the water during dough mixing, rapid cooling of baked products, and precise temperature control of the candy cooling channels. Your products will have consistent dimensions, textures, and appearances, and allow for large-scale and high-quality production.
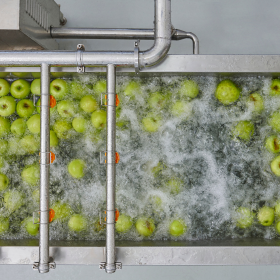
From the farm to the table, the freshness of fruit and vegetable products is their value. In the process of fruit and vegetable processing, we offer a complete set of temperature control solutions ranging from vacuum pre-cooling, water cooling, to cold chain storage. The harvested fruits and vegetables need to be rapidly cooled, which can effectively inhibit respiration, retain moisture and nutrients; the control of low temperature in the cleaning, sorting, and packaging stages can extend the processing window for you and reduce losses. This not only preservation but also maximizes the commercial value and supply radius of agricultural products for you.
See the Food Processing Chiller in Action
Watch how the food processing chiller delivers stable temperature control, fast cooling response, and reliable performance in real industrial working conditions.
Why Does the Food Processing Industry Need Chillers?
In the food and beverage industry, the demand for low-temperature environments in the production and storage stages is constantly increasing. Professional large-scale industrial chillers, as key production infrastructure, play a role far beyond just cooling. They can also establish a predictable and controllable low-temperature production environment through high-precision and stable temperature control systems. During the continuous operation of large chillers, they can efficiently remove process heat.
Choosing a reliable food processing industry is of great importance for the production and storage operations of an enterprise. It can maximize production continuity, reduce the risk of unplanned downtime, improve the utilization rate of the production line, and guarantee that every link from raw materials to final products complies with the standards, providing the enterprise with sustainable production capacity and a strong competitive advantage.
Advantages of Chillers for Food Processing
Precise Temperature Control, Ultimate Quality
The flavor, texture, and nutrition of food are highly sensitive to temperature. Our professional cooling machines offer millimeter-level temperature control, which can quickly stabilize the products in the optimal preservation state, effectively slowing down food oxidation and enzymatic reactions, and guaranteeing that the flavor and texture of your product keep unchanged from the production line to the shelves and ultimately in the hands of the consumers.
Compliant with Global Food Safety Standards
Global food safety regulations (like HACCP, FDA) have mandatory requirements for temperature control. Our chillers provide reliable and traceable temperature records, effectively inhibiting the growth of pathogenic microorganisms like Salmonella and Escherichia coli, lowering food safety risks and the possibility of product recalls, and establishing a basis of compliance trust for the brand.
Effectively Extend Product Shelf Life
Temperature is a core parameter in many food processing processes. Over time, perishable foods will naturally decompose. Through continuous and stable cooling, refrigerants can reduce the microbial activity in food and slow down the food’s own metabolic rate, scientifically extending the product’s shelf life. This not only reduces your storage and logistics losses but also provides a longer sales window.
Improve the Continuous Operation Capability of the Production Line
Stable and reliable cooling is the guarantee for continuous food production. During key processes like fermentation, coagulation, and sterilization, our chillers can precisely control the temperature, reduce downtime because of temperature fluctuations, and accelerate the production rhythm. Compared to the traditional method of continuous ice purchase, using chillers can save on high costs of consumables and labor and lower the total expenditures.
Flexible and Adaptable to Various Production Scenarios
We use an ethylene glycol anti-freezing system and redundant control to guarantee the equipment operates stably in extreme conditions, completely eliminating efficiency decline or unexpected shutdown caused by freezing. In addition, our chillers can provide customized solutions according to different food processing needs, like rapid cooling of meat, cooling of dairy products, and circulating cooling of baked products, and can flexibly adapt to your unique production processes and workshop layouts.
Our cooler can conduct precise and stable temperature control without the need for ice blocks, greatly saving on material costs and labor time.
Yes. Although an initial investment is required, by saving on energy consumption and operating costs, it usually pays off within a short period of time.
It is used for rapid cooling of food, extending its shelf life, and keeping the optimal temperature to guarantee food quality and safety.
They are mainly made of stainless steel, which is easy to clean and disinfect and fully complies with food safety and hygiene standards.


 English
 Spanish
 Arabic
 Vietnamese

